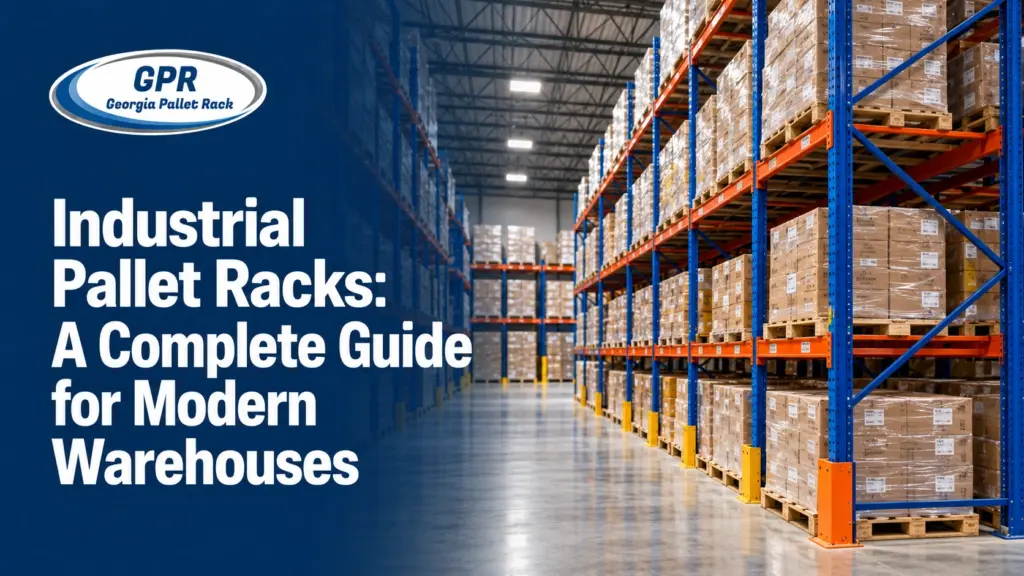
Industrial pallet racks are an important part of many modern warehouse storage plans. They help businesses organize large volumes of inventory, use vertical space, and create clearer paths for forklifts and employees. However, selecting a racking system requires more than choosing the strongest or tallest option available.
The right system depends on product weight, pallet dimensions, inventory turnover, building height, equipment, aisle requirements, and future growth. Understanding how industrial pallet racks work and what to evaluate before installation can help warehouse owners make safer and more practical storage decisions.
What Are Industrial Pallet Racks?
Industrial pallet racks are heavy-duty storage structures designed to hold palletized goods in multiple vertical levels. A typical system includes upright frames, horizontal beams, safety components, and pallet supports. These parts work together to keep stored products organized and accessible.
Unlike floor stacking, pallet racking allows warehouses to use vertical space while maintaining defined storage locations. This can improve inventory visibility and reduce the time employees spend searching for or moving products.
Common Types of Industrial Pallet Racks
Selective Pallet Racks
Selective racks provide direct access to individual pallets. They are one of the most widely used systems because they offer flexibility for warehouses with many product types, frequent inventory movement, or changing storage requirements.
The main consideration is aisle space. Selective racks may require wider aisles than high-density systems, but they make loading and retrieval relatively straightforward.
Drive-In Pallet Racks
Drive-in racks allow forklifts to enter storage lanes and place pallets several positions deep. This arrangement can increase storage density and work well for large quantities of similar products.
Because access to individual pallets is more limited, drive-in systems may not be suitable for inventory that changes frequently or requires first-in, first-out rotation.
Push-Back Pallet Racks
Push-back racks use inclined rails and carts to store pallets several positions deep. Loading a new pallet pushes existing pallets toward the back of the lane, while unloading allows the next pallet to move forward.
This design provides greater density than selective racking while allowing access from the front. It may be useful for warehouses that store multiple pallets of similar products.
Pallet Flow Racks
Pallet flow systems use rollers or wheels to move pallets through the rack. They can support first-in, first-out inventory rotation and may improve product movement in distribution, food, or high-volume storage environments.
Pallet flow racks require careful planning to match the roller design, pallet dimensions, product weight, and operating process.
Benefits of Industrial Pallet Racking
Better Use of Vertical Space
Industrial pallet racks allow businesses to store products above the floor, making better use of the building’s available height. This can increase capacity without requiring immediate expansion.
Rack height must still account for ceiling clearance, sprinkler systems, forklift reach, lighting, and building conditions. Higher storage is only useful when it can be accessed and maintained safely.
Improved Inventory Organization
A planned rack layout gives products assigned storage locations. Employees can organize inventory by category, size, turnover rate, or shipping schedule. Clear labeling and consistent placement can make picking, replenishment, and inventory counting more efficient.
Safer Material Movement
Defined rack rows and aisles can reduce congestion and create clearer travel paths for forklifts. Proper spacing also helps employees load and retrieve pallets without unnecessary movement around stored products.
How to Choose the Right System
Review Load Requirements
Determine the weight of individual pallets and the total capacity needed for each rack level. Consider the heaviest expected load rather than relying only on average product weight.
Beam length, upright height, storage levels, pallet dimensions, and load distribution all affect capacity. Load limits should be clearly marked after installation.
Measure the Facility
Review ceiling height, floor condition, structural columns, doorways, loading areas, emergency exits, and aisle widths. The layout must also provide enough room for forklifts to turn, lift, and position pallets safely.
Fire protection equipment, lighting, ventilation, and employee walkways should remain accessible. These details should be evaluated before finalizing the rack design.
Plan for Future Changes
Warehouse needs can change as inventory volume, product sizes, equipment, and order patterns develop. Modular industrial pallet racks may make it easier to add levels, rearrange bays, or expand selected sections later.
Planning for future growth can reduce the cost and disruption of replacing an entire storage system.
Installation and Maintenance Considerations
Proper installation is essential for rack stability and safe operation. Systems should be assembled correctly, anchored where required, and positioned according to the warehouse layout and equipment requirements.
Employees should be trained to load pallets evenly, follow capacity limits, and report damaged components. Regular inspections can identify bent uprights, damaged beams, missing safety pins, corrosion, or forklift impact before these issues become more serious.
Georgia Pallet Rack provides warehouse storage products and related services for businesses in Georgia and the greater Atlanta area. Its offerings include pallet racking systems, used pallet racks, pallet rack uprights, step beams, pallet supports, and row spacers. The company also provides rack installation, replacement, take-down, relocation, and custom storage solutions. For businesses planning industrial pallet racks or other warehouse systems, these products and services can support a storage plan based on inventory, equipment, available space, load capacity, and safety requirements.